Customer Focus
We make decisions based on customer requirements
and supply the necessary materials in a timely manner.
About Us
SPCI, an advanced chemical materials company since 2009.
Infrastructure
Production, research, and analytical infrastructure with 26 reactors and a total capacity of 76,450 L.
Business Model
3 collaboration models—ODM, OEM, and OBM—tailored to customer needs.
Products
36 products across metallocene catalysts, electronic materials, and specialty chemicals.
ESG Management
Sustainable management implemented through 6 policies and relevant certifications.
Information
Information on company e-brochure, our talent philosophy, employee benefits, careers, and contact information.
VISION & PHILOSOPHY
VISION
SPCI is becoming a trusted materials company through customer-focused decision-making,
continuous technological innovation, and responsible operations.
We make decisions based on customer requirements
and supply the necessary materials in a timely manner.
We enhance our competitiveness in fine chemicals
through continuous improvement and technological development.
We build lasting trust
by ensuring safety and security.
QUALITY POLICY
01
We achieve customer satisfaction by ensuring consistently reliable product quality.
02
Through continuous R&D and process innovation, we secure differentiated technological competitiveness.
03
We deliver consistent results through data-driven quality management at every stage—from the receipt of raw materials to final shipment.
We manage quality according to customer requirements
and continuously improve and develop technologies to achieve reliable material performance.
All products are inspected according to specifications agreed upon with the customer. Only products that meet those specifications are released for shipment. When conformity cannot be clearly determined, shipment is placed on hold while we consult with the customer.
We identify and manage factors that may affect product quality, minimizing batch-to-batch variation and ensuring consistent quality across initial and subsequent deliveries.
We respond promptly to quality issues, identify their root causes, and propose measures to prevent recurrence. We do not make changes without customer knowledge.
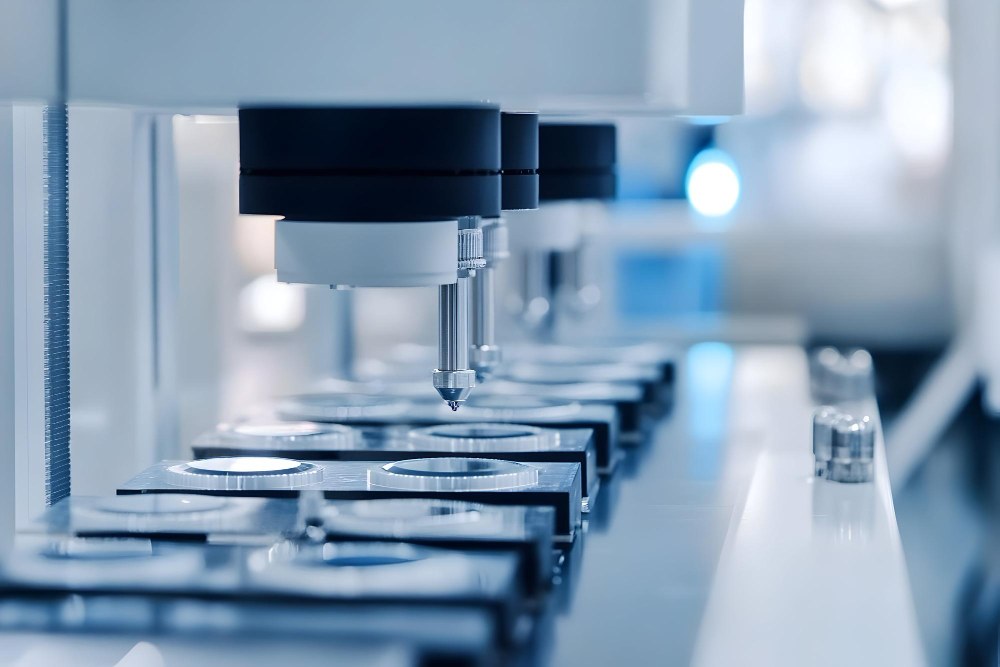
We operate in-house analytical and testing equipment, continuously improve our test methods, and provide ongoing employee training to ensure that decisions are supported by reliable data.
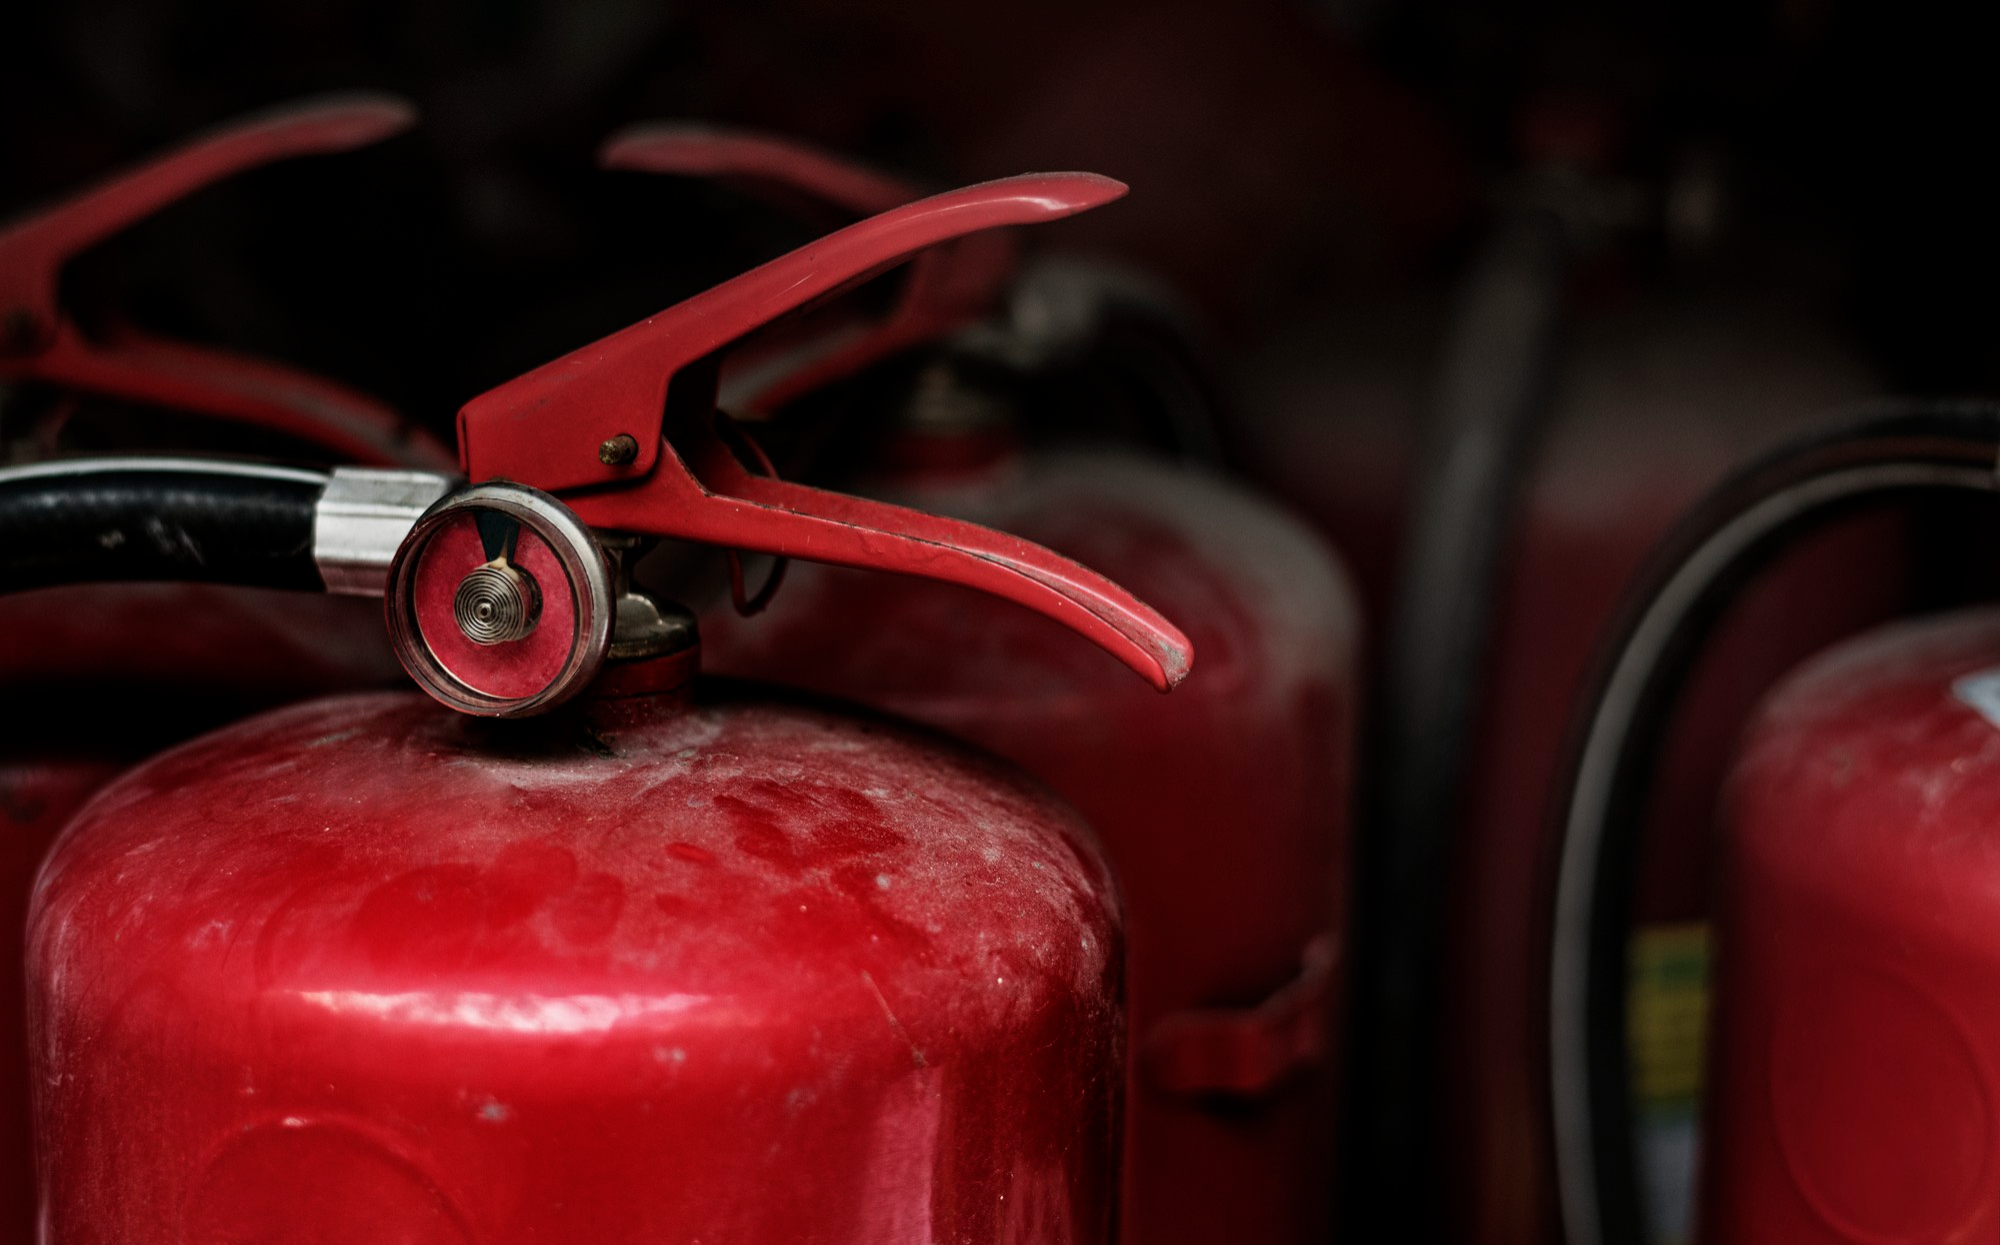
We operate specialized firefighting equipment, including dry chemical extinguishing systems and CO₂ extinguishing systems.
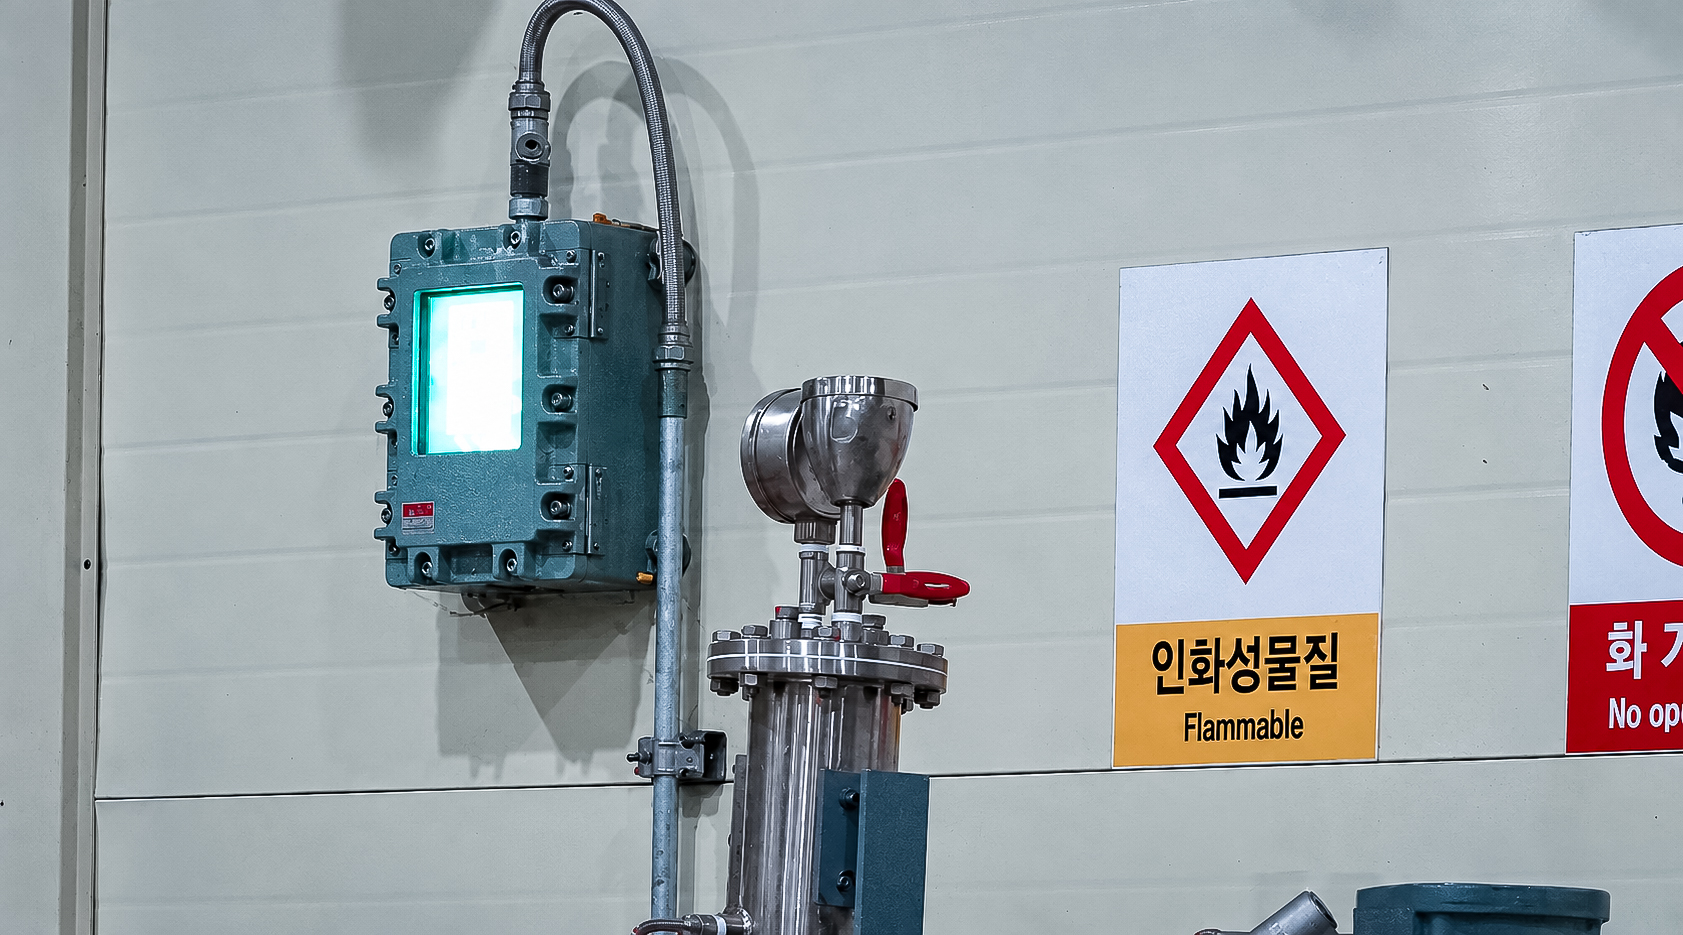
Fire and gas leak detectors are installed throughout our facilities to identify abnormal conditions early and issue immediate alerts.
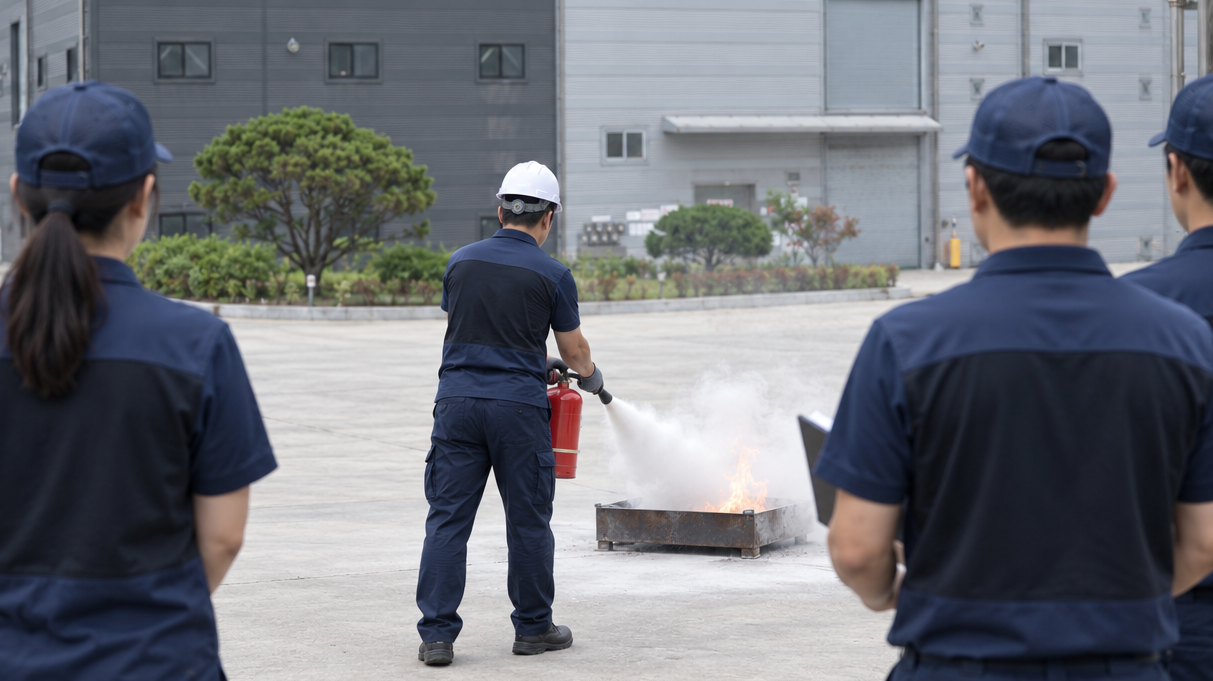
We conduct regular firefighting and emergency evacuation drills to maintain our employees’ emergency response capabilities.
SECURITY SYSTEM
SPCI systematically manages corporate assets and customer information
through integrated personnel, physical, and information security measures.
All employees sign non-disclosure agreements upon joining the company. Appropriate confidentiality agreements are also executed before work with customers begins.
We apply systematic security protocols throughout the process—from internal personnel to customer collaboration—to prevent the unauthorized disclosure of customer information and core technologies.
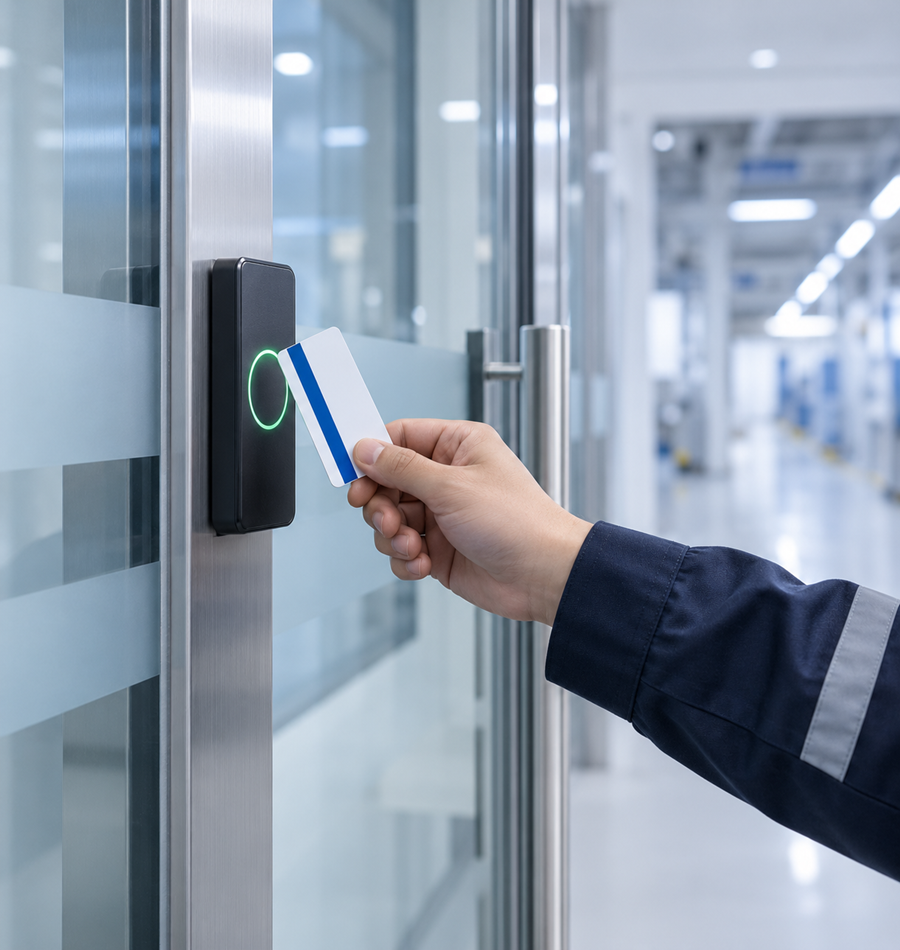
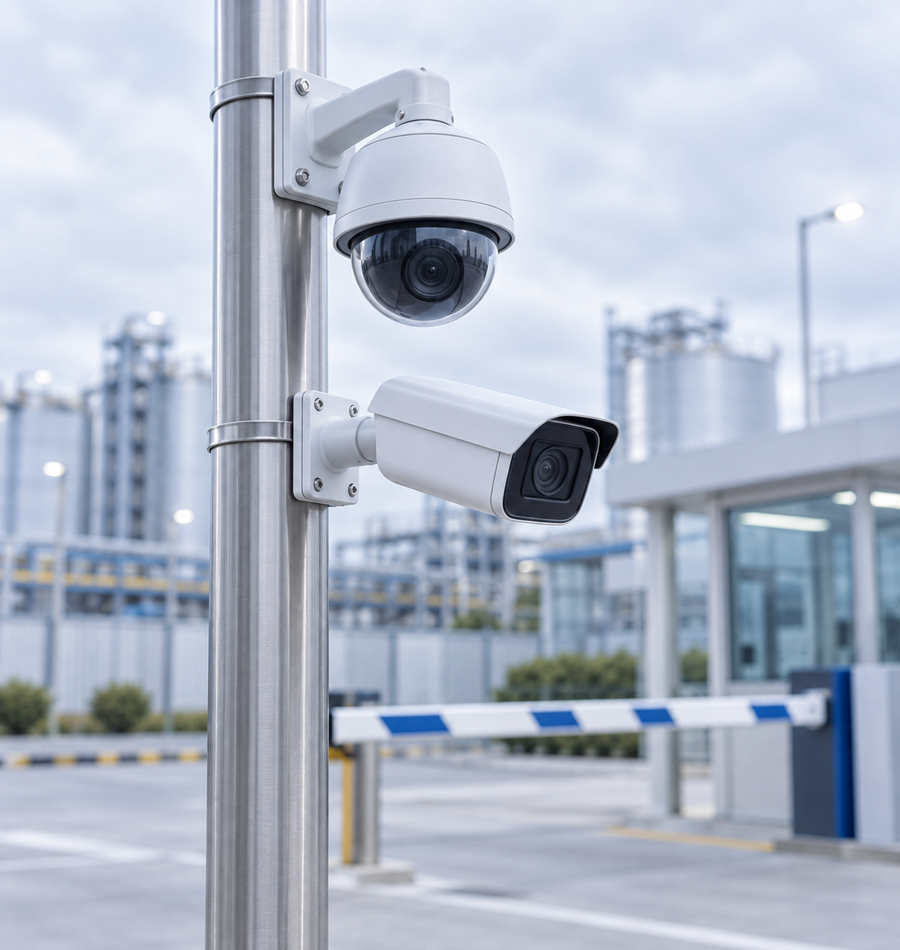
Access to major facilities is controlled through unmanned security systems and fingerprint-based authentication. Key areas within our facilities are continuously monitored using CCTV systems.
Only authorized personnel may enter restricted areas. We maintain records of on-site activities and respond promptly to security risks and incidents at our research and production facilities.
All business data is centrally managed on a server rather than stored on individual computers. User-specific permissions are assigned to control access to sensitive information.
Data storage and external transfers are subject to administrator approval, helping us securely protect customer information and core technologies.